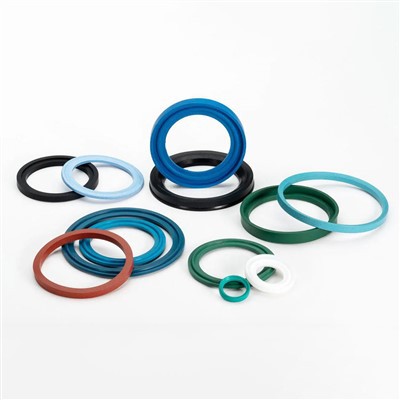
(1) Fluorine rubber: It has high temperature resistance, can be used in the environment of -30℃-+250℃, resistant to strong oxidants, oils, acids and alkalis. Usually used in high temperature, high vacuum and high pressure environment, suitable for oil environment. Due to its various excellent properties, fluorine rubber is widely used in petroleum, chemical, aviation, aerospace and other sectors.
(2) Silicone rubber: It has outstanding high and low temperature resistance, maintains good flexibility in the temperature range of -70℃-+260℃, and has the advantages of resistance to ozone and weathering. It is suitable for sealing in thermomechanics. liner. Because it has no toxicity, it can be used to make heat insulation, insulation products and medical rubber products.
3. Nitrile rubber: It has excellent resistance to oil and aromatic solvents, but it is not resistant to media such as ketones, esters and chlorinated warp. Therefore, oil-resistant sealing products mainly use nitrile rubber.
4. Chloroprene rubber: It has good oil resistance, solvent resistance, chemical media and other properties, but it is not resistant to aromatic oils. It is characterized by excellent resistance to weather aging and ozone aging. In production, neoprene is usually used to make door and window sealing strips and diaphragms and general vacuum sealing products;
5. EPDM: It has good temperature resistance, weather aging resistance and ozone aging performance. Generally, it is the most widely used in door and window sealing strips and the automobile industry.